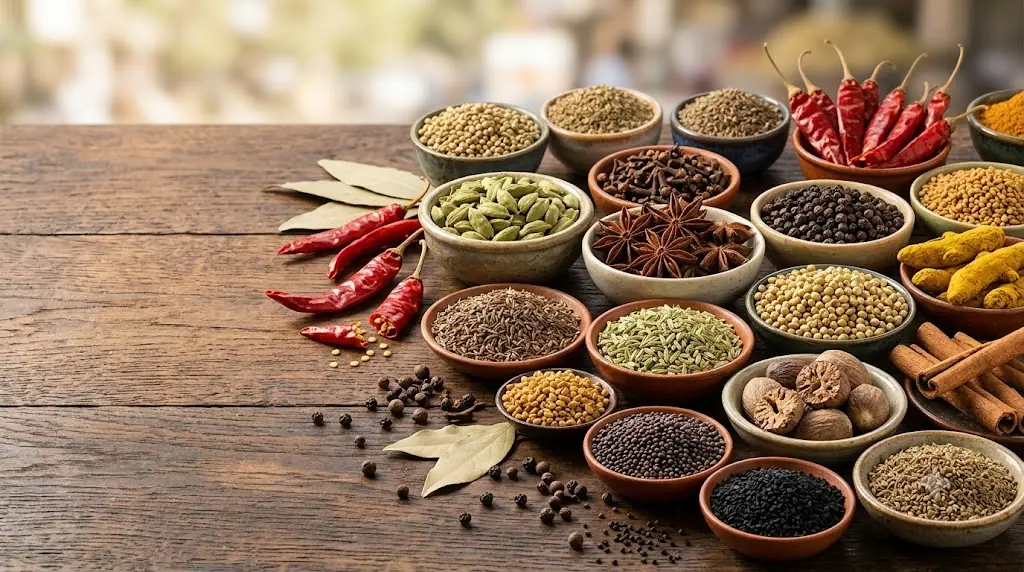
Quality Assurance for Export-Grade Indian Spices
As an Indian spices exporter and supplier, GTR International maintains strict quality control at every stage - from sourcing premium raw spices to cleaning, lab testing, packaging and export - so importers, wholesalers and food manufacturers receive the same dependable, export-grade quality in every consignment.
A comprehensive quality management system
GTR International follows a comprehensive quality management system built to deliver premium-grade Indian spices to global markets. Every batch is inspected and tested for purity, moisture and food-safety compliance before it's approved for export.
- Premium-grade raw materials
- Naturally rich aroma and flavor
- Hygienic processing environment
- Strict quality control checks
- International export standards
- Consistent, batch-to-batch quality

From farm to final delivery
Strict quality measures run across the entire supply chain, from farm to final delivery.
Raw Material Selection
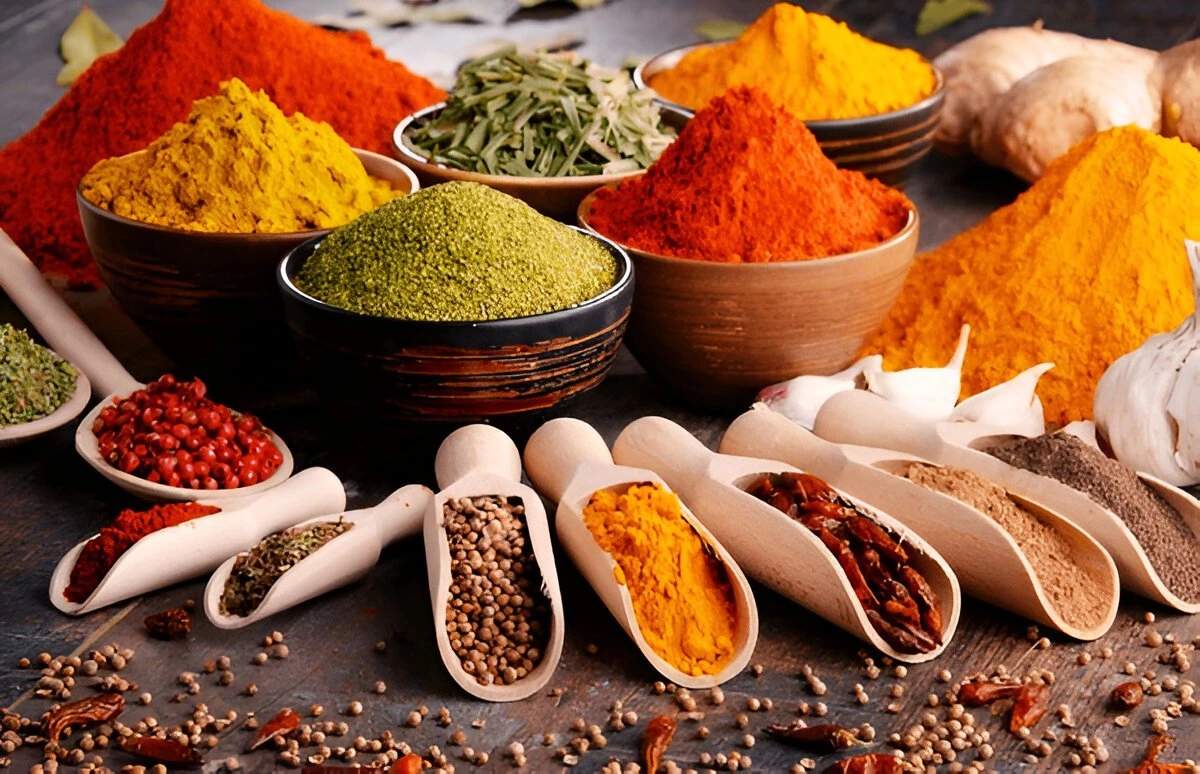
We source spices directly from trusted farmers and suppliers, selecting only produce that meets our specifications for purity, size and freshness.
Advanced Cleaning & Sorting
Modern cleaning, de-stoning and sortex-grade sorting remove impurities and deliver uniformity, purity and premium quality.
Laboratory Testing
Every batch is tested for quality parameters, moisture, purity and food-safety compliance before approval - the testing that keeps shipments clearing inspection at destination.
Secure Packaging & Export
Products are packed in food-grade, export-ready materials that preserve freshness, aroma and shelf life through long-distance international transport.
Facilities built around food safety
Our modern facilities uphold the highest standards of food safety, hygiene and product integrity.
Hygienic Processing Units
Strict hygiene protocols and best practices protect product purity and safety.
Quality Inspection Systems
Dedicated teams inspect at every stage of processing and packaging.
Advanced Cleaning Technology
Modern machinery delivers effective cleaning, grading and sorting.
Food Safety Compliance
Aligned with internationally recognized food-safety standards and destination-market requirements.
Controlled Storage Facilities
Temperature-controlled storage preserves freshness and quality until dispatch.
Export-Ready Packaging
Durable, secure packaging protects products during long-distance shipping.
Ready to Source Premium Indian Spices?
Tell us the product, grade and destination - our export team will share availability, pricing and samples.